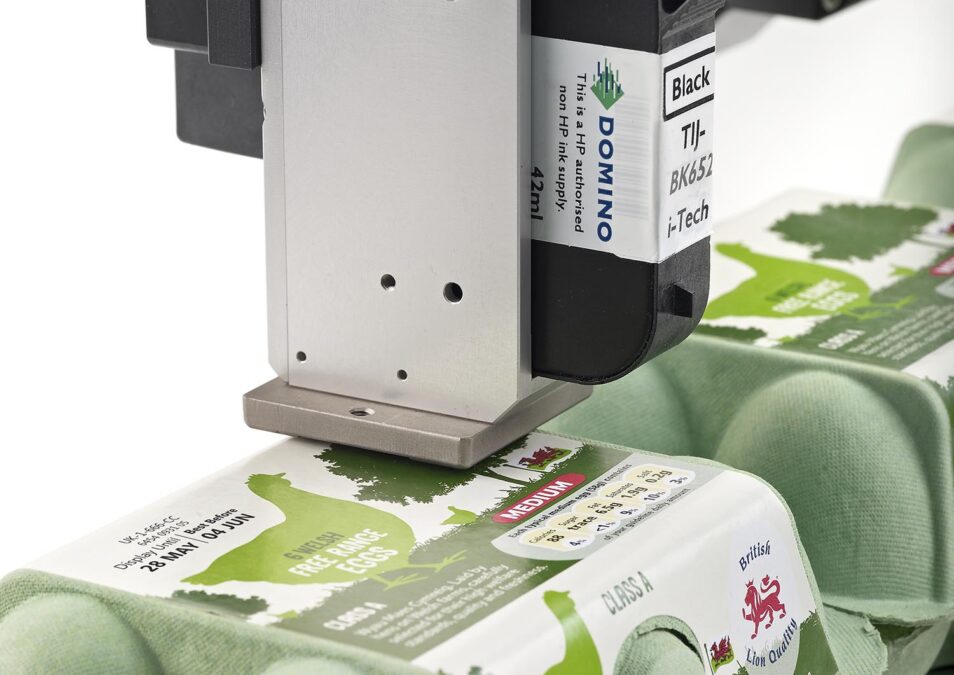

Egg cartons vary widely in shape and material. A label that bonds to a smooth plastic lid may bridge the fibers of molded pulp, and a code placed across a lid hinge may tear when the carton opens. Test the exact carton and refrigerated route used by the producer.
Measure the Lid After Closing
Molded pulp lids can have raised lettering, ventilation openings, and uneven corners. Measure the truly flat area on a filled, closed carton. Position the barcode away from a ridge or closure tab. If a required label is larger than the flat panel, redesign the package band rather than folding a code over the edge.
Check Pulp and Plastic Separately
Pulp fibers and plastic coatings provide different contact surfaces. Request adhesive samples for each carton type and inspect both initial tack and bond after refrigeration. Dust from pulp forming or condensation on plastic can alter results. A single room-temperature peel test cannot represent both routes.
Keep Variable Dates Controlled
Print lot and date data from the packing system and verify the first carton after each flock, lot, or packing-day change. Remove old label stock or templates when date logic changes. A barcode can scan perfectly while the printed date is wrong, so the quality check must inspect both data and print.
Test Opening and Stacking
Stack cartons as retailers and delivery drivers do, then open and close a sample several times. Check whether a label tears at the lid edge, rubs against the carton above, or hides a defect. Scan the code under retail lighting after the cold interval. Record performance by carton manufacturer when packaging is sourced from more than one plant.
Define the Job Before Choosing Stock
Write down exactly what the label on egg cartons must accomplish during packing, refrigerated distribution, and retail display. Decide which field a worker reads, which code a scanner captures, and when the information can be retired. The working data may include pack date, lot, grade or size where applicable, and inventory code; distinguish fields that must be printed from those better kept in the inventory system. Decide who owns an incorrect record and how it is corrected. A label specification based only on dimensions misses the process that gives the printed mark its meaning.
Match Adhesive to the Real Surface
Test the proposed adhesive on molded pulp and smooth plastic cartons, using the exact material supplied to production. Apply it at the normal work area temperature and inspect it after the planned dwell, not only after a few minutes. The main challenges here are rough pulp, curved lids, condensation, and stacking. A stronger adhesive may hold better but can create residue or damage during removal. If direct application is unreliable or undesirable, assess a preprinted wrap band with a variable-data area. Keep approved samples from each packaging or carrier supplier so a later material substitution triggers a targeted retest.
For this application, compare egg carton labels on the actual molded pulp and smooth plastic cartons and through the planned handling interval. Ask for samples before choosing a full production roll.
Choose the Roll and Printer Together
Confirm print width, label height, gap or black-mark sensing, roll core, outside diameter, winding direction, and printer feeding limits before ordering. A roll that shares the same face dimensions can still jam or print backwards if its core or winding is wrong. Use the production template and print a long enough run to reveal feed drift, adhesive ooze, or die-cut variation. Record the approved printer settings with the roll specification. Recheck them when a device, converter, or template changes.
Make Every Scan Deliberate
Design the barcode for the scanner and distance used with egg cartons. Leave the required clear margin, preserve contrast, and keep the code away from folds, seams, edges, or moving parts. Put the most useful human-readable identifier beside it so staff can spot a mismatch. If more than one code appears on the object, state which workflow uses each one and remove obsolete routing codes. Print the longest data value and smallest label in the test set; a short sample code can hide layout problems.
Apply the Label at a Repeatable Point
The preferred position is a flat lid panel that does not cross the opening edge. Apply only after the object or package has reached the form it will have during normal handling. Remove loose dust or moisture where the process permits, press across the entire label, and check the corners. Give workers a simple placement guide showing the approved zone and the areas to avoid. If the application surface changes between suppliers or batches, check a few finished units before the shift continues. An attractive label applied in the wrong place is still a failed label.
Run a Trial That Mirrors Use
Print a production roll and test it on the hardest version of egg cartons, then follow it through packing, refrigerated distribution, and retail display. Check printer feed, initial readability, adhesion, edge lift, and scanning at each real handoff. Include the worst expected combination of rough pulp, curved lids, condensation, and stacking. Keep both successful and failed examples with the time and conditions recorded. If a sample fails, change one factor at a time, such as placement, adhesive, size, or print settings. This makes the result useful for purchasing rather than a vague pass or fail.
Control Reprints and Old Labels
A torn label, wrong template, or corrected record needs an explicit replacement path. Reprint from the verified current record, not from memory or a photograph of the old label. Where identifiers are unique, preserve the link to the original record and mark a failed print as void if the system supports it. Remove or cover an obsolete active code so a scanner cannot select the wrong one. Document who authorizes a new label when the physical item and the digital record disagree.
Give the Supplier an Approval Specification
Send a sample of molded pulp and smooth plastic cartons, the printer model, a dimensioned label drawing, roll geometry, required data and barcode layout, expected life, and the environmental conditions described above. Ask for converted-roll samples of the proposed construction. Agree on the acceptance test before a bulk order, including feed performance, scan success, bond after normal handling, and removal behavior when relevant. Record the approved material, adhesive, liner, die cut, and winding as one controlled specification. Compare cost per successfully labeled unit rather than only the blank-label price.
When evaluating direct thermal labels for egg cartons, give the supplier the real surface, printer details, and pass criteria rather than a size alone.